Article Directory
- 1 What Is a Non-Standard Screw Prototype?
- 2 The Five-Stage Prototype Development Process
- 3 Material Selection Decides Prototype Performance
- 4 Lead Time and Cost Drivers in Prototype Cycles
- 5 Prototype vs. Production: What Changes Between Runs
- 6 How to Evaluate a Non-Standard Screw Prototype Supplier
- 7 Frequently Asked Questions
An outdoor actuator bracket failed at 1,200 hours in a salt-spray chamber, and the cause was a standard screw with the wrong head geometry and an unprotected shank. The fix required a non-standard screw prototype: a custom head, a modified thread runout, and 316 stainless steel. Eleven working days later, the sample passed torque-to-failure testing, and the production order followed directly from the approved prototype. For engineers and purchasing teams, that sequence is the real value of the prototype development process: it converts an untested drawing into a measurable, approved part before a single production batch is committed.
Zhejiang Donghe Machinery Technology Co., Ltd., a fastener manufacturer based in Jiashan County, China, applies the same logic to every custom fastener it ships. The company produces GB, DIN, ANSI, and BS standard products, and its non-standard business starts where those standards stop. Understanding how the company builds a non-standard screw prototype helps buyers evaluate suppliers, control cost, and know which drawings are actually ready for machining.
What Is a Non-Standard Screw Prototype?
A non-standard screw prototype is a pre-production sample machined from a custom drawing to verify geometry, material, and performance before a full production run.
Definition
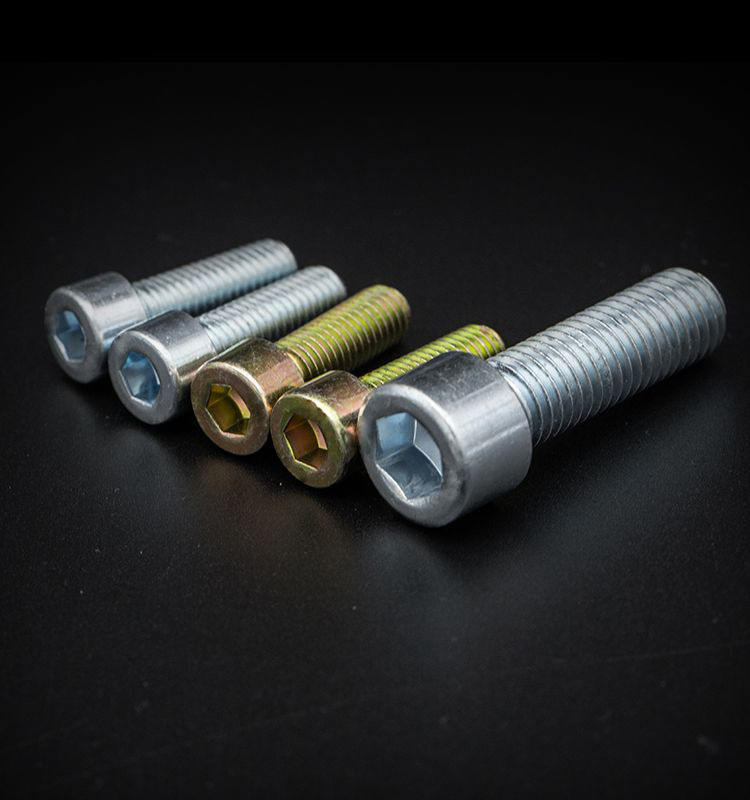
A non-standard screw is a threaded fastener that does not conform to GB, DIN, ANSI, or BS standard dimensions, designed to meet a specific head shape, thread, length, material, coating, or performance requirement.
Prototypes exist because a drawing is not proof of function. Head height, drive recess depth, thread pitch, fillet radius, and coating thickness all interact with the mating part; only a physical sample can confirm that the screw installs correctly and holds the specified clamp load.
Typical triggers for a prototype request include:
- A standard catalogue screw fails on head height or drive recess geometry
- Thread engagement demands an unusual pitch or a multi-start thread
- The material must resist a specific corrosive or high-temperature environment
- Assembly requires a one-piece geometry that replaces a bolt-and-nut stack
The prototype stage is also the cheapest point to change the design. A machined non-standard screw prototype can be modified with one new setup, while a production die cannot. That is why experienced suppliers push for a complete drawing review before the first chip is cut.
 Custom DIY Industrial Mechanical Fasteners Manufacturers, Factory, ExportersZhejiang Donghe Machinery Technology Co., Ltd. is China DIY Industrial Mechanical Fasteners Manufacturers And OEM/ODM DIY Industrial Mech...View Product →
The Five-Stage Prototype Development Process
The non-standard screw prototype development process follows five defined stages, and every stage produces a written record that the production team can scale from.
- Application and load analysis. Define the material stack, clamping force, exposure environment, and assembly torque before any drawing work begins.
- Drawing and tolerance review. Confirm thread class, head undercut, fillet radius, and coating thickness on the drawing; the prototype must reflect the drawing exactly.
- Material and coating selection. Match the substrate to corrosion and strength demands, and choose a coating for galvanic compatibility and friction behavior.
- CNC tooling and machining. Turn, mill, or thread-roll the geometry with box tools and dedicated form tools; a prototype batch is normally fewer than 50 pieces.
- First-article inspection and functional test. Measure critical dimensions, verify hardness and tensile properties, and run tests such as torque-to-failure or pull-out load.
The difference between prototype failure and production failure is cost. A prototype that fails the assembly test costs a few machining hours. A production run that fails the same test costs a whole order.
The drawing stage deserves the most attention. Designing non-standard bolts for industrial applications requires clear callouts for thread runout, underhead fillets, and coating base-material tolerance — details that are rarely visible in a 3D model but always visible in a failed test.
Material Selection Decides Prototype Performance
Material selection is the single largest factor in prototype cost, corrosion resistance, and mechanical performance.
| Material | Typical application | Strength and cost profile |
| Carbon steel (10B21, 1022) | General machine prototypes | Low cost; requires zinc or galvanic coating for corrosion |
| 304 stainless steel | Indoor and mild outdoor use | Strong and economical; the default choice for most prototypes |
| 316 stainless steel | Coastal, marine, chemical environments | Higher pitting resistance; roughly 30–40% higher material cost |
| Alloy steel (SCM435, 40Cr) | High-strength structural bolts | Needs heat treatment and hydrogen embrittlement control |
| Titanium and aluminum | Lightweight and aerospace fastening | Long machining time; premium prototype cost |
316 stainless steel costs roughly 30–40% more than 304 in raw material, but it delivers substantially higher pitting resistance in chloride exposure. When the prototype must survive a marine environment, the extra cost is justified at the drawing stage, not after salt-spray failure.
The same geometry can behave differently across alloys. A hardened carbon-steel prototype with a zinc flake coating suits a tight-tolerance dry assembly, while the same screw in 316 stainless may gall under repeated torque. The right call depends on the application, not on price alone. Suppliers that ask about the environment before quoting are already reducing your prototype iterations. Guidance such as alloy selection for corrosive environments is part of the review a serious manufacturer runs before machining.
For buyers, this is also the stage to confirm material certificates. A custom non-standard bolt prototype service should provide test certificates with the sample, not only with the production batch.
Custom Non-Standard Bolt Manufacturers, Factory, ExportersZhejiang Donghe Machinery Technology Co., Ltd. is China Non-Standard Bolt Manufacturers And OEM/ODM Non-Standard Bolt Factory, We Custom ...View Product →Lead Time and Cost Drivers in Prototype Cycles
Typical non-standard screw prototype lead times run from 3 to 6 weeks, and four factors determine most of the variance.
3–6 wk
Typical prototype lead time from drawing to tested sample
±0.05 mm
Common machining tolerance on critical prototype diameters
5–7 days
Typical tooling preparation for CNC turning of a custom head
2–4x
Per-piece cost of a prototype compared with a production screw
The chart below shows a realistic breakdown of a 23-working-day prototype cycle for a turned non-standard screw in stainless steel.
Cost follows the same logic: material grade, tooling, batch size, heat treatment, and coating each drive the per-piece price. Buyers can compare realistic ranges from manufacturing lead times for non-standard bolts, but the final quote depends on how completely the drawing defines the part. An incomplete drawing costs more than the missing tolerance values — it costs an extra prototype cycle.
Prototype vs. Production: What Changes Between Runs
A prototype proves the design; production proves the process, and the two are governed by different cost and tolerance logic.
Prototype run
- Quantity of 1 to 50 pieces
- Shared CNC tooling with box tools and form tools
- Tolerances of ±0.05 mm achievable with individual measurement
- High per-piece cost; every part can be inspected
- Acceptance based on first-article report and functional test
Production run
- Quantity of 10,000 pieces and above
- Dedicated dies, thread-rolling, and automated feeding
- Tolerances held by process control and statistical sampling
- Low per-piece cost after tooling amortization
- Acceptance based on batch inspection and process capability
A prototype that cannot be replicated at production volume is not a finished design. The supplier should flag features that force hand operations or second-setup machining before the prototype is approved — those features will be the first thing to break in mass production.
This is why the prototype drawing must be production-aware. A head type that is easy to turn on a CNC lathe but difficult to form in a heading die will add cost for the life of the product. Reviewing the prototype with the production process in mind saves far more than machining time.
How to Evaluate a Non-Standard Screw Prototype Supplier
Evaluate a non-standard screw prototype supplier on drawing response speed, inspection capability, and material traceability, not on price alone.
- Asks about the application environment and assembly torque before quoting
- Returns a manufacturability review with a tolerance and coating plan
- Provides material certificates and heat-treatment records with the sample
- Runs in-house dimensional inspection and shares the first-article report
- Can handle export documentation and international logistics
The prototype functions as a contract between the design office and the factory floor. An incomplete first-article report means incomplete production risk — request the full inspection record with every sample.
Zhejiang Donghe Machinery Technology Co., Ltd. supports the workflow with a stated annual capacity above 8,000 tons, more than 100 machines, and an in-house inspection laboratory. The company exports to Europe, Australia, Africa, and the United States, so the prototype process includes the export documentation that overseas buyers need before a production order moves.
For geometries that do not fit a normal head-and-shank layout, such as special keys, offset heads, or multi-diameter shanks, special-shaped bolt prototype development follows the same five-stage process but with more time reserved for CNC programming and custom form tools.
 Wholesale Special-shaped bolt Suppliers, ManufacturersWe Wholesale Special-shaped bolt, Zhejiang Donghe Machinery Technology Co., Ltd. Is China OEM/ODM Special-shaped bolt Suppliers And Manuf...View Product →
Frequently Asked Questions
How long does a typical non-standard screw prototype take?
Most prototype cycles run from 3 to 6 weeks, depending on material availability, heat treatment, and coating. A turned stainless steel screw with a standard head style can commonly be sampled in 3 to 4 weeks; unusual alloys or complex multi-diameter geometry extend the schedule.
What drawings or samples do I need to provide for a prototype quote?
Send a drawing with thread class, head type, length, tolerance, material, and coating, or a physical sample for reverse measurement. The more precisely the drawing defines thread runout, underhead fillet, and critical diameters, the fewer prototype iterations you will pay for.
What is the minimum order quantity after the prototype is approved?
The minimum depends on the production process. Thread-rolled and headed parts normally require 10,000 pieces or more to justify tooling; CNC-machined geometries can be produced in smaller quantities, though per-piece cost will be higher.
How do I choose between 304 and 316 stainless steel for a prototype?
Use 304 for indoor and mild outdoor environments where cost matters. Choose 316 when the screw will face salt water, coastal air, or chemical exposure, because the higher molybdenum content provides substantially better pitting resistance for a 30–40% material cost premium.