Article Directory
- 1 The Manufacturing Route in Brief
- 2 What Makes a Screw "Non-Standard"?
- 3 Material Selection: The First Quality Decision
- 4 Wire Preparation and Cold Heading: Forming the Blank
- 5 Machining and Secondary Operations: Where the "Non-Standard" Appears
- 6 Thread Rolling: Building Strength While Forming the Thread
- 7 Heat Treatment and Surface Finishing: Performance in Service
- 8 Inspection, Tolerances and Traceability
- 9 Cost and Lead-Time Realities
- 10 Conclusion
The Manufacturing Route in Brief
Imagine a replacement screw for a European machine: M8 x 1.25, an 80 mm shank, a reduced head height and a corrosion-resistant finish. The drawing looks ordinary, but no DIN, ISO, GB or ANSI series covers that combination. That is when the question changes from "which screw do I buy?" to "how is this screw made?"
The short answer: non-standard screws are manufactured through a six-stage route: material selection, wire preparation and cold heading, machining of special features, thread rolling, heat treatment and surface finish, and final inspection. The difference is not the amount of engineering; it is the amount of control at every step.
- Select material and confirm mechanical properties.
- Draw and prepare wire or bar stock.
- Cold-head or machine the blank.
- Roll or cut the thread.
- Heat-treat and apply surface finish.
- Inspect dimensions, hardness and coating.
What Makes a Screw "Non-Standard"?
A non-standard screw is any fastener that does not conform to a published standard series in dimensions, thread form, tolerance, material or head style. In practice, most custom fasteners are not exotic shapes. They are common geometries with one or two deliberately changed parameters: a longer shank, a finer pitch, an altered head height, a special drive, or a tighter tolerance.
Standards such as DIN, ISO, GB, ANSI and BS define baseline dimensions and mechanical properties. When an engineer leaves that baseline, the manufacturer must interpret the drawing, select the right starting material and decide how the features will be formed. That is why custom non-standard screw design considerations need to be settled before production begins.
Typical non-standard variations
- Head diameter, height or angle changed from series values
- Custom drive systems or mixed drive and head combinations
- Thread pitch or diameter outside the standard range
- Extended or reduced shank length
- Special point styles such as flat tail, dog point, or pilot point
- Non-standard material grades or hybrid coatings
Material Selection: The First Quality Decision
Material determines how easily the blank can be formed, how strong the finished screw will be, and how long it will survive in service. Low and medium carbon steel covers the majority of commercial fasteners. Alloy steel is used when higher strength is required. Stainless steel, brass, aluminium and titanium are chosen for corrosion resistance, conductivity, weight or appearance.
Before any forming begins, the wire or bar must be checked for composition, surface defects and diameter. For non-standard screws, this step matters more than for standard parts because the later operations are built around the actual material properties.
How material changes the process
| Material | Typical use | Effect on processing | Corrosion behaviour |
|---|---|---|---|
| Carbon steel | General industrial fasteners | Easy cold heading and thread rolling | Low unless coated |
| Alloy steel | High-strength joints | Requires heat treatment after forming | Low unless coated |
| Stainless steel | Outdoor, marine, food contact | Work-hardens faster; needs more forming force | Good, but grade dependent |
| Brass and aluminium | Electrical and low-load applications | Soft and easy to machine; less suitable for high torque | Good in mild environments |
| Titanium | Aerospace, chemical, medical | Difficult to form; lower speeds and special tooling | Excellent corrosion resistance |
For chemical and aerospace work, titanium non-standard screws are a clear example of material driving the process. The forming speed, tool material and lubricant all change compared with steel.
 Wholesale Plain Titanium Hex Bolt M12 x 80mm Suppliers, ManufacturersWe Wholesale Plain Titanium Hex Bolt M12 x 80mm, Zhejiang Donghe Machinery Technology Co., Ltd. Is China OEM/ODM Plain Titanium Hex Bolt ...View Product →
Wire Preparation and Cold Heading: Forming the Blank
Almost all screws start as coiled wire rod or straight bar stock. The manufacturer first draws the wire to the exact shank diameter, then cleans and coats it with a lubricant carrier. This preparation prevents galling and die wear during cold forming.
In cold heading, a cut-off die shears a length of wire, and a series of punches and dies in a multi-station former upsets the metal to create the head and sometimes the shank shape. This is the heart of high-volume screw production. A custom non-standard screw manufacturing project uses the same principle, but the dies are designed for the custom geometry.
 Wholesale Non-standard screw Suppliers, ManufacturersWe Wholesale Non-standard screw, Zhejiang Donghe Machinery Technology Co., Ltd. Is China OEM/ODM Non-standard screw Suppliers And Manufac...View Product →
Cold heading is preferred because it preserves the metal grain flow and strengthens the head. It also produces almost no material waste. However, it is not suitable for every custom shape. A very large head, an extremely thin section, or a brittle material may require machining instead of forming.
Machining and Secondary Operations: Where the "Non-Standard" Appears
After blank forming, the next operations create features that cold heading cannot achieve alone. CNC turning can reduce a shank diameter, cut undercuts or produce precise head geometry. Milling or slotting creates drive recesses, cross holes or wrench flats. Flat-tail screws, for example, need a machined end face so the screw can seat flush against a fixture or rail.
A pan-head flat-tail non-standard screw shows how a simple-looking design often combines cold heading with a secondary milling operation. The head is formed, then the tail is machined to deliver the exact flat surface.
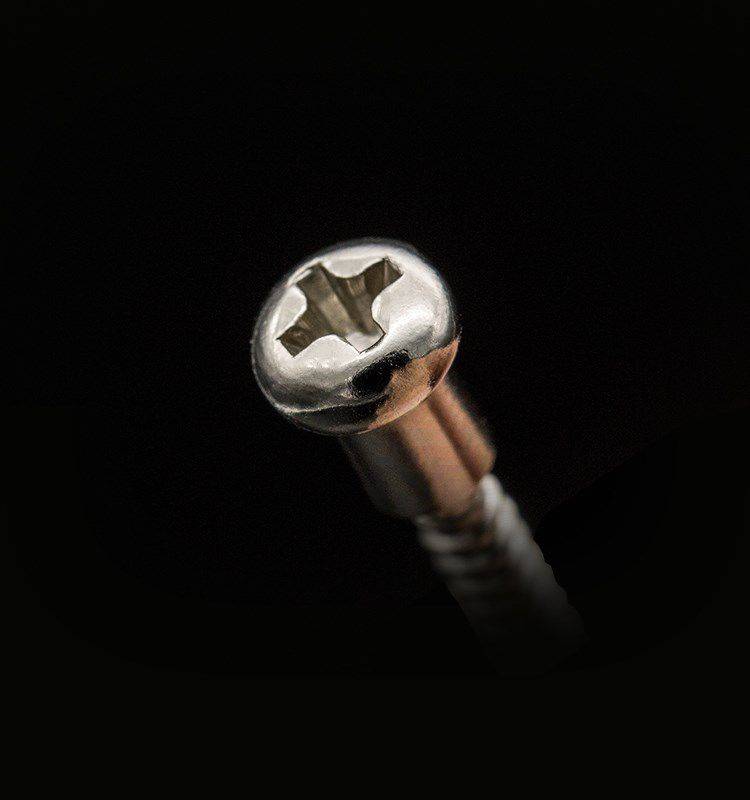 Wholesale Pan head flat tail non-standard screw Suppliers, ManufacturersWe Wholesale Pan head flat tail non-standard screw, Zhejiang Donghe Machinery Technology Co., Ltd. Is China OEM/ODM Pan head flat tail no...View Product →
Common secondary operations
- CNC turning for shank diameters and stepped profiles
- Milling for slots, recesses and special head shapes
- Drilling for cross holes or lubrication grooves
- Grinding for high-precision bearing surfaces or tight concentricity
When machining replaces cold heading
Small quantities below the minimum for a custom die set are often machined from bar stock. The same is true for very large diameters, hardened materials that cannot be formed, and threads with awkward profiles. Machining increases unit cost but removes the need for expensive tooling and allows faster design changes.
Thread Rolling: Building Strength While Forming the Thread
Most non-standard screw threads are produced by rolling, not cutting. The blank is pressed between hardened dies whose profiles squeeze the metal into the thread form. This process displaces the material, so the grain flow remains continuous around the thread roots. The result is a stronger thread with a smooth, work-hardened surface.
Thread rolling works well for standard pitches, and it also works for custom pitches when the die can be made economically. If the pitch is very coarse, square, or outside the practical rolling range, the thread is cut on a lathe. Cutting is more flexible for low volumes but produces a slightly weaker thread because the grain lines are interrupted.
Tolerance is decided here. A non-standard pitch can be made to a normal 6g or 6h class, or to a tighter custom range, but each option has cost consequences. The thread die cost is one reason non-standard thread forms usually have a minimum order quantity.
Heat Treatment and Surface Finishing: Performance in Service
As-formed carbon steel has limited strength. For most non-standard fasteners, a quench-and-temper cycle raises hardness and tensile strength. Alloy steel grades respond predictably to heat treatment, but geometry matters: sharp corners, drilled holes and thin sections can become brittle if hardness is pushed too high.
Heat treatment choices
- Quench and temper for medium and high carbon steels
- Case hardening for low-carbon screws that need a hard surface and tough core
- Selective hardening when only the thread or driving area must be hard
Surface finishes
- Electroplated zinc with clear or coloured passivation
- Hot-dip galvanizing for thicker outdoor protection
- Zinc-flake coatings for extended salt-spray performance
- Black oxide for improved appearance and light protection
- Nickel or brass plating for electrical and decorative uses
Surface finish is not cosmetic only. It determines salt-spray performance, installation torque and assembly compatibility. High-strength steel fasteners also need a hydrogen-embrittlement bake after acid cleaning or electroplating. This is one of the most important quality checks in the process.
Inspection, Tolerances and Traceability
The real cost driver in non-standard screws is usually inspection, not machining. A standard screw is covered by a known standard, so the customer and manufacturer already agree on dimensions and test methods. A custom screw has no such shortcut. Every dimension has to be defined, measured and documented.
A serious manufacturer will run a first-article inspection before mass production. They will check shank diameter, overall length, thread pitch, head angle, drive depth, hardness and coating thickness. This requires a fastener manufacturer that can hold complex tolerances and provide the inspection data in a usable format.
For critical applications, traceability from the wire heat to the final batch becomes part of the order. That means the material certificate, heat-treatment records and inspection reports stay aligned with the screw lot number.
Cost and Lead-Time Realities
Non-standard does not automatically mean expensive. It means the cost structure is different from standard production. You are not paying for a stock item; you are paying for engineering interpretation, special tooling, process trials and more inspection time.
- Quantity has the largest influence; a custom die set needs enough pieces to spread its cost.
- Tight tolerances require more measurement time and more scrap risk.
- Heat treatment and surface finish add process steps, but they also add reliability.
- Material choice affects forming speed, tool life and the final price per piece.
The typical lead time and cost factors for non-standard screws include drawing review, tooling production, first-article approval and the production run itself. A generous target: for a moderate quantity, expect several weeks from drawing to delivery.
Conclusion
Non-standard screws are not mystery parts. They follow the same manufacturing logic as standard fasteners, but they demand earlier design alignment, better tooling and stricter inspection. If you can answer the material, tolerance, volume and finish questions in the first conversation, the manufacturing process becomes predictable.