Article Directory
- 1 What Makes a Screw Non-Standard and Why CNC Machining Fits
- 2 The CNC Machining Process for Non-Standard Screws
- 3 Material Selection for CNC-Machined Non-Standard Screws
- 4 Tolerances, Thread Classes, and Surface Finish
- 5 Quality Control During CNC Production
- 6 Cost Drivers and Design for Manufacturability
- 7 How to Work with a CNC Screw Manufacturer
- 8 Final Thoughts on CNC Machining for Non-Standard Screws
When a client sends us a drawing for a screw that has no DIN, GB, ANSI, or BS equivalent, the first question is not whether we can make it. It is how precisely and how quickly the CNC machining process can turn a raw bar into a functional fastening part that fits their assembly, resists the operating environment, and survives repeated loading. For non-standard screws, CNC machining is often the only practical route when volumes do not justify dedicated tooling or when geometry pushes beyond what cold heading can produce.
In this guide, we walk through the CNC machining process for non-standard screws, the material and tolerance decisions that matter, and the quality checks that separate a usable screw from a recurring equipment failure. Whether you are a design engineer, a purchasing manager, or a maintenance planner, these are the factors that determine success.
What Makes a Screw Non-Standard and Why CNC Machining Fits
A non-standard screw is any fastener that does not conform to the dimensional, thread, material, or head-style conventions of standard fastener families. It may use an unusual thread pitch, a custom shank length, a security drive, an oversized flange, or a feature that only exists on a proprietary design. Standard screws are typically cold headed because volume justifies the tooling. Non-standard screws often arrive in smaller quantities, with tighter tolerances, and in grades of stainless steel, titanium, or high-strength alloy that are difficult to form.
CNC machining removes this constraint. Because cutting tools are guided by a digital program, there is no dedicated die to build and no hammering force to limit the shape. A machining centre or turning centre can produce a screw with an undercut, a retention groove, a milled flat, or a steep point without compromising cycle time. The trade-off is unit cost at high volumes, which is why the decision between cold heading and CNC depends on your quantity and geometry.
Cold Heading vs. CNC Machining at a Glance
| Factor | Cold Heading | CNC Machining |
|---|---|---|
| Ideal volume | High volume (over 50,000 parts) | Low to medium (1 to 20,000 parts) |
| Geometric complexity | Limited to formable shapes | Nearly unlimited with 5-axis capability |
| Material range | Mostly low to medium carbon steels | All steels, stainless, titanium, brass, aluminium |
| Setup cost | High (dies and headers) | Moderate (programming and tooling) |
| Tolerances | Good, but limited by die wear | Excellent, consistent within microns |
For a custom screw with a unique head shape or a thread tolerance class that cold heading cannot hold, CNC machining is the more reliable path. You can also machine screws as a finished part in one chucking, eliminating the secondary operations that add cost and lead time. If you are exploring a custom geometry, the starting point is often a general specification such as our custom non-standard screw family, which can be adapted to your drawing rather than forcing a standard onto your design.
 Wholesale Non-standard screw Suppliers, ManufacturersWe Wholesale Non-standard screw, Zhejiang Donghe Machinery Technology Co., Ltd. Is China OEM/ODM Non-standard screw Suppliers And Manufac...View Product →
The CNC Machining Process for Non-Standard Screws
Every CNC screw starts as a round bar or hex bar. The process is not simply turning down a diameter; it is a sequence of operations that builds the head, thread, point, and any secondary features while holding tolerances that affect both assembly and strength.
1. Material Preparation and First Operation
The selected rod is cut to length or fed automatically from a bar loader. The machine faces the end, centres the part, and turns the shank and thread-major diameter. For screws with a shank tolerance in the range of h8 or h9, this first operation locks the baseline for every subsequent feature.
2. Head and Drive Formation
Depending on the design, the head is formed by turning, milling, or a combination. Slotted, Phillips, Torx, hex, and square drives can all be produced with the appropriate tool, but the under-head geometry is often most critical: a load-bearing face that must be perpendicular to the shank to avoid bending stress. A chamfer or fillet under the head reduces stress concentration. Examples like pan-head flat-tail designs show how a simple head change can affect seating and stripping behaviour, as covered in our range of pan-head flat-tail non-standard screws.
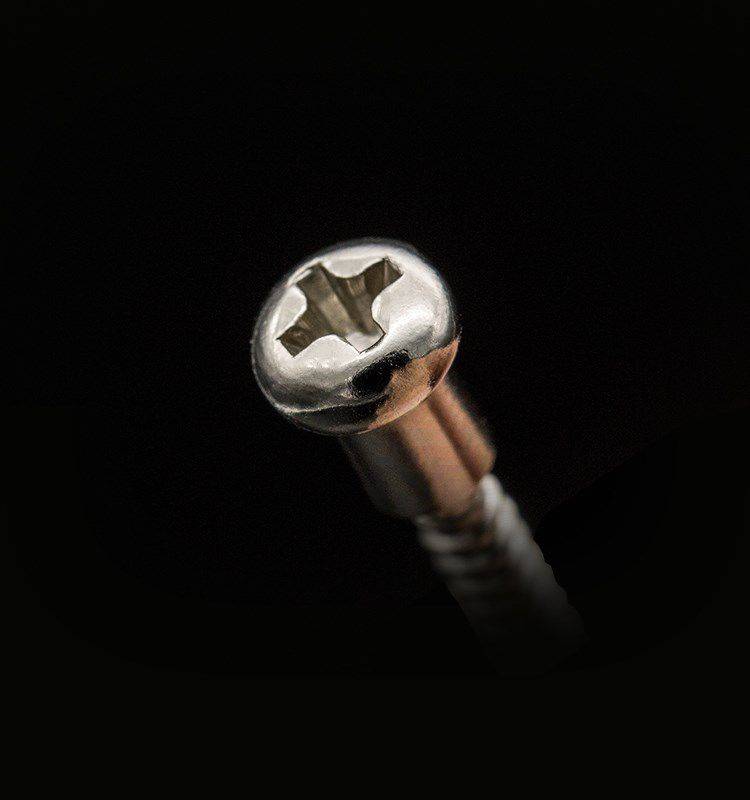 Wholesale Pan head flat tail non-standard screw Suppliers, ManufacturersWe Wholesale Pan head flat tail non-standard screw, Zhejiang Donghe Machinery Technology Co., Ltd. Is China OEM/ODM Pan head flat tail no...View Product →
3. Thread Cutting vs. Thread Whirling
Non-standard threads are cut, milled, or whirled on a CNC machine. Single-point threading is flexible but slower for long threads. Thread milling is the best choice when the thread runs close to a shoulder or when the material is hard. Whirling, common on Swiss-type lathes, removes material rapidly and produces excellent finish for long screws. Rolling, in contrast, is usually reserved for standard pitches and enough batch size to justify the rolling head investment.
For a custom thread pitch, confirm the tolerance class. Common metric classes such as 6g for external threads and 6H for internal nuts still apply to non-standard screws. If your drawing specifies a different class, the CNC program simply shifts the tool path; there is no need to modify a die.
4. Point, Undercut, and Tail Features
Points are produced by turning or milling. A conical point, a chamfered point, a dog point, or a self-drilling point changes the cutting tool geometry. Undercuts and retention grooves can be machined to exact widths. These details affect how the screw starts, drives, and locks. It is also where a design intended for automated assembly needs the most careful tolerance control.
5. Finishing and Surface Treatment
After cutting, the screw is deburred, cleaned, and prepared for plating, passivation, hot-dip galvanizing, or other coatings. CNC machining produces a consistent surface, but edge burrs on a non-standard screw can still lead to thread gauging failures. Controlled deburring is not a formality; it is part of the geometry. This is where a high-spec design can benefit from a titanium-grade material that requires no coating for corrosion resistance, such as the titanium non-standard fasteners we offer.
 Wholesale Plain Titanium Hex Bolt M12 x 80mm Suppliers, ManufacturersWe Wholesale Plain Titanium Hex Bolt M12 x 80mm, Zhejiang Donghe Machinery Technology Co., Ltd. Is China OEM/ODM Plain Titanium Hex Bolt ...View Product →
Material Selection for CNC-Machined Non-Standard Screws
Material affects machining speed, tool wear, corrosion performance, and mechanical strength. The table below shows typical choices and why they matter.
| Material | Typical Grade | Why Choose It | Common Application |
|---|---|---|---|
| Carbon steel | 1010, 1045 | Low cost, machinable, can be hardened | General industrial assembly, painted or plated finishes |
| Alloy steel | SCM435, 4140 | High strength, good fatigue resistance | Automotive and heavy equipment fastening |
| Stainless steel | 304, 316 | Corrosion resistance, biocompatibility | Food equipment, marine, medical devices |
| Titanium | Ti-6Al-4V or CP2 | Lightweight, high strength, corrosion resistant | Aerospace, racing, high-end assemblies |
| Brass | H59, H62 | Electrical conductivity, low friction | Electrical terminals, decorative hardware |
| Aluminium | 6061, 7075 | Lightweight, easy machining | Electronic enclosures, brackets |
From a machining standpoint, the three factors that matter most are machinability, the final surface treatment, and whether you require a stress-relieved or hardened core. A CNC process can hold fine threads in stainless steel, but it will require slower speeds and better coolant. Titanium requires rigid setup and proper tool geometry. Brass and aluminium are forgiving but generate different chip control and finish requirements. If you already have a material performance target, communicate the standard you expect, such as ISO or ASTM, because a non-standard fastener still needs a defined material baseline.
Tolerances, Thread Classes, and Surface Finish
The most common mistake in non-standard screw drawings is over-specifying tolerances that add cost without improving function. A shank diameter of 6 mm with a tolerance of ±0.05 mm may be enough for a locating feature, while the same diameter may need ±0.013 mm to work as a sliding pin. A CNC machining centre can hold both, but the tighter tolerance wastes cycle time in measurement and tooling consistency.
On drawings, you should define the thread tolerance class in the callout, for example M8 x 1 – 6g. If the screw engages a tapped hole, specify the class of fit. For head and shank concentricity, a typical requirement is 0.05 mm total indicated runout (TIR). Surface roughness usually comes from the drawing symbol; Ra 3.2 is acceptable for most screws, Ra 1.6 for seating faces, and Ra 0.8 only for functional surfaces such as a bearing shoulder.
Our experience with parts that require reliable manufacturing of non-standard fasteners with complex tolerances shows that the tolerance only works if it is measurable on the shop floor. A drawing that calls for an optical dimension that no gauge can reach will lead to disagreement during inspection. Use callouts that your supplier can verify with standard micrometers, thread gauges, and profilometers.
Quality Control During CNC Production
Quality control for non-standard screws starts with first-article inspection, not the final batch. The operator or inspector verifies all critical dimensions on the first piece before continuing. During production, sampling plans like ISO 2859 are common, but high-value aerospace or medical parts often justify 100% inspection of key dimensions.
The measurement equipment depends on the feature: thread plug gauges and ring gauges confirm fit; a micrometer or laser scan checks diameters; a profile projector or optical comparator checks head form and point angle; a surface tester checks roughness. For material integrity, hardness testing and salt spray tests verify heat treatment and coating quality. If the drawing requires a special coating thickness, that is also measured and documented.
At our facility, a dedicated inspection team and laboratory support both source inspection and in-house verification. We document the actual values, not just a pass/fail mark, so your incoming quality audit has the records it needs. For products used in structural or safety applications, this traceability is a requirement, not an option.
Cost Drivers and Design for Manufacturability
CNC machining cost for a non-standard screw is driven by material, programming, setup, cycle time, inspection, and surface treatment. The unit price drops as quantity increases because setup and programming are spread over more pieces. A rule of thumb is that a complex part with 3 axes of milling will cost more than a simple turned part, but a design that can be produced in one clamping can be surprisingly economical.
The best way to control cost is to review the drawing before it is released. Remove unnecessary tight tolerances. Reduce the number of thread starts or reliefs if possible. Choose a standard blank size. And specify a finish that matches the environment. If you are early in the design phase, our design guidance for non-standard bolts explains what geometry has the most impact on manufacturability.
Also consider the total landed cost, not just the piece part price. A screw that fails in the field costs far more than one with an extra chamfer. If you are comparing quotes from multiple suppliers, ask for the exact lead time and cost factors so you can compare like with like.
How to Work with a CNC Screw Manufacturer
Start with a complete drawing or sample. A 3D model is useful, but a 2D drawing with tolerances and surface finish symbols is what controls the manufacturing contract. If you only have a sample, be prepared to trust your supplier for reverse engineering; make sure they measure it first and confirm the material before cutting.
Tell the supplier what the screw does. A screw that holds a bracket in a static indoor assembly has different requirements from a screw that vibrates, carries shear load, or sees saltwater. The performance context influences material, coating, and inspection level.
Plan for a sample phase. Most non-standard screw orders include several pieces for fit testing. Use that phase to verify thread fit, head seating, and insertion torque. Once the sample is approved, the production run can proceed with confidence. A manufacturer with in-house machining and inspection can compress this loop, which is why we keep both the process and the gauging in the same plant.
Final Thoughts on CNC Machining for Non-Standard Screws
CNC machining is the most flexible and reliable route to a non-standard screw that has to meet engineering requirements. It supports complex geometry, tight tolerances, high-performance materials, and small batches that cold heading cannot justify. The key is to define your requirements clearly, invest time in a measurable drawing, and work with a supplier that can demonstrate both machining capability and quality control.
If you are evaluating a non-standard screw design, start with the geometry, material, and thread class, then assess the cost and lead time. A well-executed CNC part will usually outlast a modification of a standard part and will very likely make your assembly simpler. Get the process right, and you will never have to settle for a “close enough” fastener again.